Table of Contents
How Online Manufacturing Sourcing Works Today
If you are an engineer or procurement professional sourcing custom sheet-metal parts, you have more options than ever. Online manufacturing platforms let you upload CAD files, receive quotes, and order parts — sometimes within minutes. But behind the web interface, these platforms operate under different business models. Some own the factory floor. Some broker orders to a network of third-party shops. Some are directories that connect you to suppliers without managing the transaction at all. The model behind the platform directly affects your unit cost, quality consistency, communication experience, and what happens when something needs to change mid-production.
Quick answer: A source factory owns the equipment and the factory floor that makes your parts, rather than brokering orders to partner shops or reselling capacity. That means one contract, one quality system and direct pricing. WERIX manufactures sheet metal parts in its own 3,000+ sqm facility in Dongguan, China.
The WERIX Model: One Factory, Full Control
WERIX Metal is a source factory. That term gets used loosely in this industry, so here is what it means specifically for us: every machine on our 3,000+ sqm production floor is owned and operated by WERIX. Every engineer on our team is a WERIX employee. Every quality check from incoming material inspection to final shipment audit happens in our facility, on our equipment, by our people. When you order sheet-metal parts from WERIX, your parts move through our own laser, punch, brake, weld, and finishing cells in sequence — all under one roof, all covered by a single purchase order. There is no third-party handoff, no routing to an anonymous subcontractor, and no markup between you and the production line.
- Founded in 2015 in Dongguan, Guangdong — 11+ years of continuous sheet-metal and stamping operation
- 3,000+ sqm manufacturing space with 5 dedicated production workshops under one roof
- 5,000+ clients served across 30+ countries and 14 industries
- 98% on-time delivery rate
- Flexible order quantities — from single prototypes to 100,000+ piece production runs
What "In-House" Means in Practice
When we say all processes are in-house, that covers the full sheet-metal sub-process chain and a complete stamping operation — not just cutting and bending. Here is what runs on our floor every day:
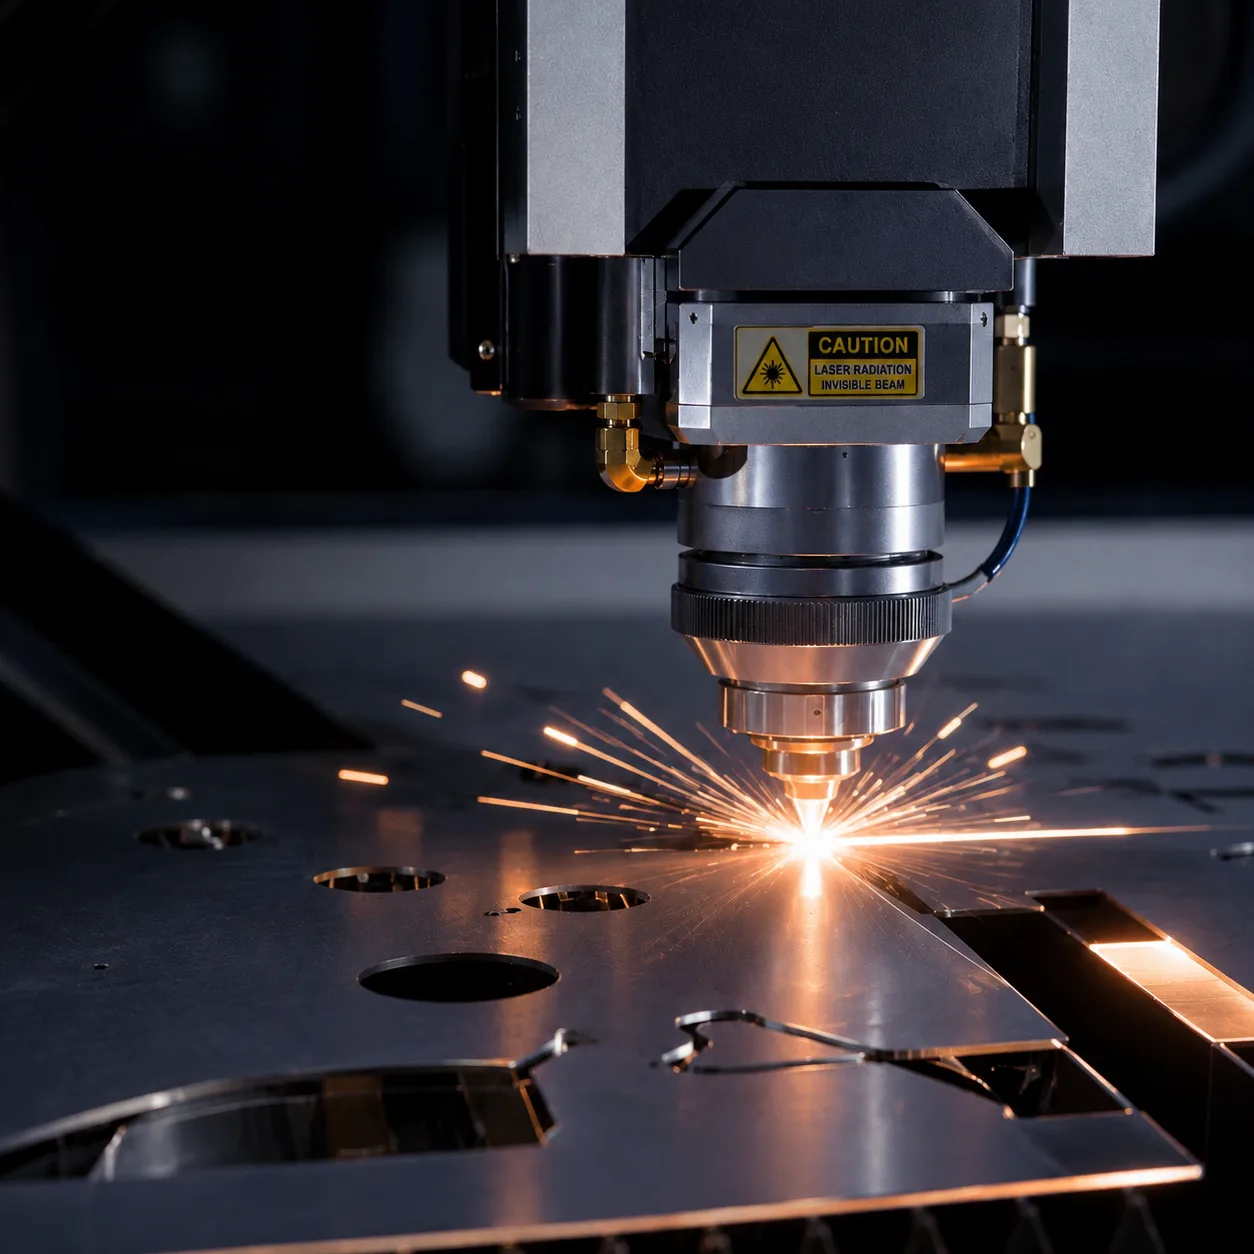
Our two fiber laser cutting machines are a DNE 3000W and a Hans Laser 6000W. DNE LASER (迪能激光) is a wholly owned subsidiary of the Swiss Bystronic Group, and the 6 kW unit from Han's Laser (大族激光) gives us the headroom for thicker stainless and aluminum work without changing the setup.
| Process | Equipment | Key Specifications |
|---|---|---|
| Fiber Laser Cutting | DNE 3000W (dual-pallet exchange) + Hans Laser 6000W | 0.3–5.0 mm, ±0.1 mm, 1500×3000 mm bed |
| CNC Turret Punching | 72-tool turret | 500 hits/min, 3.0 mm min hole diameter |
| CNC Press Brake Bending | TOPSEN TR/TM 10030 | 3100 mm bending length, ram positioning ±0.02 mm, backgauge repeatability ≤0.02 mm |
| Precision Shearing | CNC backgauge | 4000 mm max cut, 0.01 mm resolution |
| TIG Welding | Manual, full penetration | Zero spatter; food-grade / sanitary surfaces welded to AWS D18.1 practice |
| MIG Welding | Semi-automatic | 2–3× faster deposition, enables IP65-rated sealed enclosures |
| Spot Welding | Resistance welder | 0.1 s per spot, no filler material |
| Laser Welding | Fiber laser source | HAZ under 1 mm, seam width 0.2–2 mm |
| Metal Stamping | 25T–300T presses, in-house die shop | Progressive, transfer, deep-drawing; 200 strokes/min |
Stamping die fabrication — wire EDM, CNC grinding, and die tryout — happens in our own die workshop. Our standard progressive tooling is designed for 1,000,000+ strokes in typical applications — actual die lifetime varies by material, thickness, and part complexity. Because the die is built and tested on the same floor where it runs production, there is no shipping, no fitting mismatch, and no third-party finger-pointing if something needs adjustment.
Quality System: Four Stages, One Floor
Quality in a source factory works differently from quality in a broker model. When the same team that builds your parts also inspects them, problems are caught at the workstation — not after the parts ship. Our four-stage quality process covers every production batch:
- Stage 1 — Incoming Material: each batch of raw sheet is checked for thickness, grade certification, and surface condition before it enters production
- Stage 2 — In-Process Check: first-article inspection plus statistical random sampling at every workstation — laser, bend, weld, stamp
- Stage 3 — Final Inspection: dimensions verified against your drawing with precision instruments (CMM, calipers, micrometers). Tight-tolerance parts receive Zeiss CMM scanning with full GD&T validation
- Stage 4 — Shipment Audit: packaging, labeling, surface protection, and batch traceability confirmed before dispatch
"Full material certs and FAI reports included — exactly what we needed for medical device quality management system certification compliance. Passed incoming inspection first time." — Lisa, Quality Assurance Lead. "Inspection report was included without us asking." — Pierre, R&D Engineer, France. Our first-pass yield on standard tolerance parts (±0.1 mm) stands at 98%+.
Engineering Support That Knows Your Parts
Every project at WERIX is assigned a single dedicated engineer who follows your order from the first sample to mass production. This is the same person who reviews your DFM, answers your questions during sampling, and supervises your parts during the production run. If a bend radius needs adjusting or a tolerance is tighter than necessary, your engineer catches it before cutting starts — not after.
- Pre-production DFM review covers: minimum bend radius, flange length, hole-to-edge distance, tolerance feasibility, and finish compatibility
- Your engineer provides a marked-up report with specific callouts — not generic automated checklists
- Design revisions are handled iteratively: upload a revised file, get updated pricing within hours
- For complex assemblies, the engineer reviews the full BOM for process consolidation and cost-down opportunities
"Pre-production DFM suggested increasing the bend radius on critical edges, which avoided cracking." — Pierre, R&D Engineer, France. "DFM feedback flagged a sharp radius that would have cracked — recommended 2 mm with a 3× bend radius. Their engineering team actually understands sheet metal." — Tom, Manufacturing Engineer, Germany.
How Different Sourcing Models Compare
The table below outlines the key differences between the three main sourcing models. Each model serves a different need — understanding which one fits your project is more useful than assuming one is universally better.
| Dimension | Source Factory (WERIX) | Online Platform / Marketplace | Supplier Directory |
|---|---|---|---|
| Who owns the equipment? | We do — 100% owned and operated | Varies — some own, some subcontract | N/A — directory only |
| Who makes your parts? | Our team, on our floor | Platform or network supplier | Supplier you contact directly |
| Quality control | 4-stage in-house QC, same facility | Platform standards, supplier-managed | No platform QC |
| Engineering support | Dedicated engineer per project | Platform-based project management | Direct with supplier |
| Communication | Direct to production engineer | Through platform interface | Direct with supplier |
| Pricing | Factory-direct, no middle layer | Platform pricing (includes margin) | Supplier-set pricing |
| Assembly & multi-process | All under one PO — PEM, weld, coat, pack | May require separate vendors | You coordinate separately |
| IP protection | Single named factory under NDA | Depends on platform policy | Depends on supplier |
| Quote turnaround | Within 24 hours | Seconds to hours | 2–5 business days per supplier |
| Minimum order | No MOQ for sheet metal | Varies by platform | Varies by supplier |
The simplest test of a source factory is a factory walk-through on video. Request a live factory call, or upload a drawing to get a direct-from-factory quote within 24 hours.
Standards referenced: an in-house quality system is only meaningful if it is certified. WERIX operates to ISO 9001, with material certification to ASTM A480/A480M for stainless grades.
FAQ
Written by
Senior Process Engineer
Tom has spent more than a decade on the shop floor turning drawings into parts that run right the first time. He leads DFM reviews at WERIX Metal, sets the bending and tooling strategy for every new project, and writes the guides engineers actually reach for when they are sizing a part late at night.
View profileParts we make for this topic
Ready to Start Your Project?
Get DFM feedback and a quote within 24 hours. No minimum order quantity.